

Key Criteria for Choosing a Reliable Narrow Aisle Reach Truck Manufacturer
Release time: 2026-07-27
Table of Contents
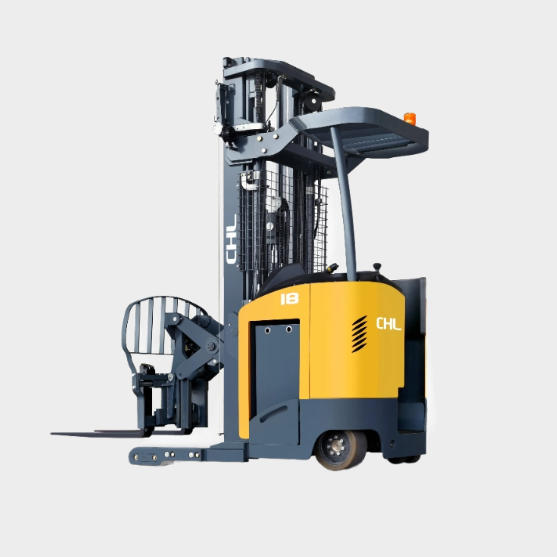
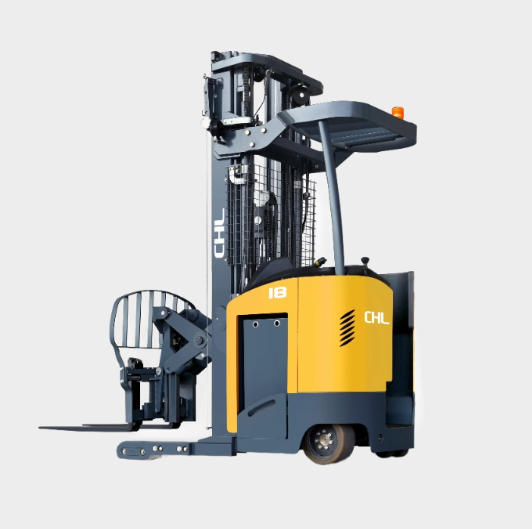
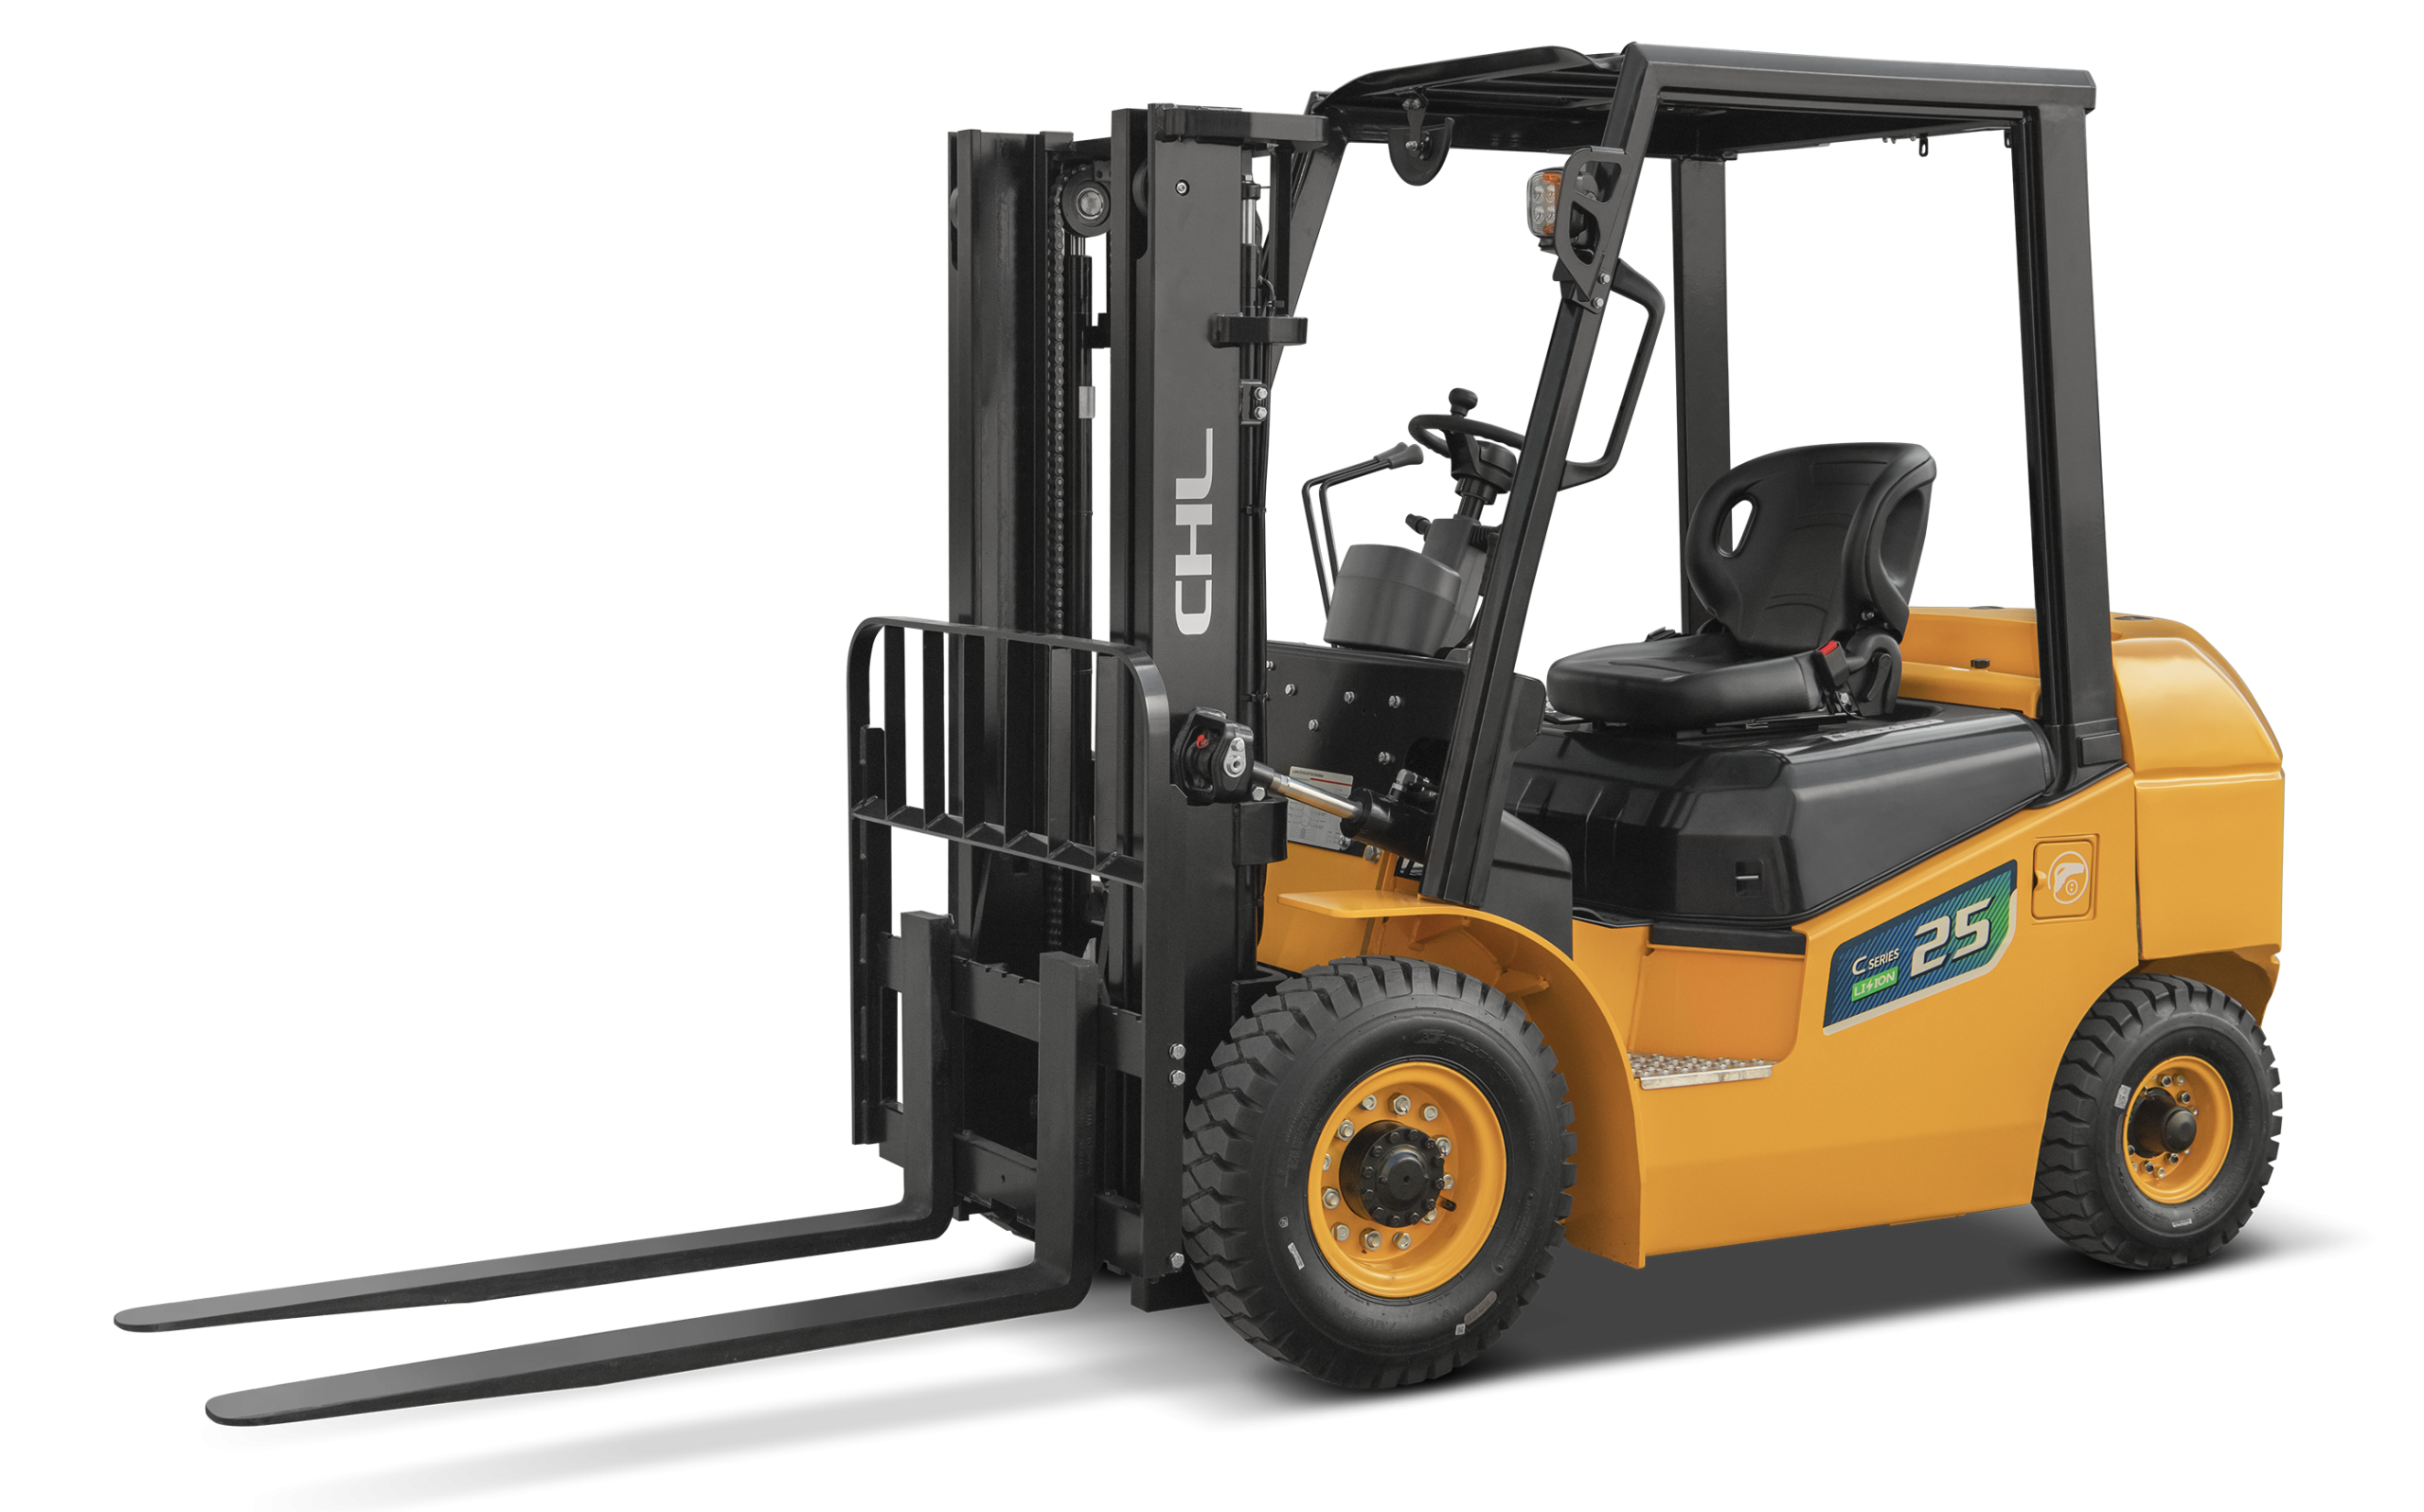
As high-density and intensive warehousing continues to develop, the narrow aisle reach truck has become a key material-handling solution for businesses looking to maximize warehouse space, improve high-level pallet stacking efficiency, and reduce warehouse operating costs.
Compared with conventional counterbalanced forklifts, these trucks are designed for demanding warehouse environments characterized by narrow aisles, high storage heights, frequent operation, and precise handling requirements. As a result, they place significantly higher demands on structural design, electronic control systems, safety protection, and application adaptability.
When selecting equipment, businesses should evaluate manufacturers comprehensively across key areas such as technical R&D, manufacturing capabilities, quality control, customized solutions, and full-lifecycle service. Choosing a reliable direct manufacturer can help ensure long-term stable, efficient, and safe equipment operation while maximizing the value of the warehouse equipment investment.
1. In-Depth Expertise in Narrow Aisle Applications and Dedicated R&D Capabilities
The operating environment of a narrow aisle reach truck is highly specialized. Warehouse aisles are significantly narrower, stacking heights can typically reach 6–12 meters, and operations often involve frequent starting, stopping, steering, and positioning.
The combination of confined spaces and high-level handling places much greater demands on equipment stability, precision, and safety than conventional forklift applications. This specialized operating environment also creates a technical barrier that general forklift manufacturers may find difficult to overcome.
A reliable manufacturer should have a dedicated R&D system and independent technical capabilities, particularly in three key areas.
First, structural optimization technology is essential. Manufacturers should have expertise in mast anti-sway technology, vehicle center-of-gravity optimization, and rigid frame design to address common challenges such as high-level load movement, positioning deviations, and rollover risks.
Second, independent electronic control system development is important. A high-precision control system designed for narrow aisle applications should provide smooth low-speed positioning, intelligent speed limitation, and precise starting and stopping, helping operators achieve highly accurate handling in confined aisles.
Third, power system adaptation is necessary for demanding operating conditions. For high-frequency continuous operation, long standby periods, and low- or high-temperature warehouse environments, manufacturers should optimize lithium battery systems, energy consumption, and power output logic to prevent performance degradation during frequent operation.
Professional manufacturers should also continue investing in technological development and hold patents covering structural design, electronic control, and safety protection. They should be able to optimize equipment parameters according to factors such as rack height, aisle width, floor flatness, and operating frequency, ensuring that the truck is properly adapted to demanding high-density warehousing environments.
2. Standardized Precision Manufacturing, Strict Quality Control, and Compliance Certifications
Narrow aisle reach trucks are specialized material-handling equipment, and their stability directly affects warehouse operating safety as well as the safety of racks, goods, and personnel. Mature manufacturing processes and strict quality control are therefore fundamental to product reliability and important indicators of a trustworthy manufacturer.
From a manufacturing perspective, a qualified manufacturer should establish a closed-loop quality control system covering the entire production process. This should include core component selection, precision machining, vehicle assembly, dynamic commissioning, high- and low-temperature testing, and overload safety testing, with standardized procedures controlling every stage.
Key components such as the electronic control system, mast assembly, traveling mechanism, and hydraulic system should use high-quality configurations rather than low-grade replacement parts. This helps ensure reliable operation during long-term, high-frequency use while minimizing the risks of component failure, structural deformation, and hydraulic leakage.
In terms of compliance, manufacturers should hold the required nationally recognized special equipment manufacturing licenses and follow internationally recognized management standards such as ISO 9001 for quality management, ISO 14001 for environmental management, and ISO 45001 for occupational health and safety management.
Products should also meet applicable international safety requirements, such as CE and ISO 13849, and manufacturers should be able to provide complete third-party testing reports and certificates of conformity. These qualifications help ensure compliance with industrial warehousing safety requirements and reduce potential equipment and regulatory risks from the outset.
3. Scenario-Based Customization and Integrated Warehouse Solutions
Narrow aisle requirements vary significantly between industries and warehouse environments.
For example, e-commerce warehouses may require high-frequency short-distance handling, cold-chain facilities may involve low-temperature and high-humidity conditions, automotive parts warehouses may require heavy-load high-level stacking, while fine chemical warehouses may prioritize quiet and clean operations.
A standardized forklift model cannot necessarily meet all of these requirements. Manufacturers that only sell standard equipment may therefore struggle to support more sophisticated warehouse operations. The key advantage of a professional manufacturer is the ability to develop scenario-based, customized, and integrated material-handling solutions.
Professional manufacturers can provide engineering support throughout the project lifecycle. During the initial stage, engineers can conduct on-site assessments and accurately evaluate critical parameters such as clear aisle width, rack height, floor load capacity, operating routes, and average daily workload.
Based on these measurements, the manufacturer can then customize the equipment configuration by optimizing vehicle dimensions, mast height, load capacity, steering angle, and safety features.
For specialized applications, additional functions may be configured, including low-temperature protection, noise and dust reduction, fast battery replacement, and intelligent collision prevention.
At the later stage, manufacturers can also provide professional guidance based on the company’s warehouse planning, including equipment selection and configuration, warehouse operation optimization, and human-machine coordination strategies.
This approach helps ensure that the equipment is properly matched to the actual warehouse environment and can improve overall material-handling and warehouse turnover efficiency.
4. Comprehensive Full-Lifecycle Service for Reliable Equipment Operation
Narrow aisle forklifts are often critical equipment for high-frequency warehouse operations. Once a truck experiences unexpected downtime, inbound storage, outbound handling, and pallet stacking operations can be disrupted, potentially resulting in significant financial losses.
For this reason, after-sales response time, maintenance capabilities, and spare parts availability are important indicators of a manufacturer’s overall strength. These service capabilities are almost as important as the quality of the equipment itself.
A trustworthy manufacturer should establish a comprehensive service system covering the entire equipment lifecycle.
First, a rapid after-sales response mechanism is essential. Service locations and technical support should be available to provide timely assistance and emergency repair services, minimizing equipment downtime as much as possible.
Second, sufficient genuine spare parts inventory should be maintained. Core components should be readily available to avoid parts shortages, compatibility problems associated with substitute components, and unnecessarily high repair costs, thereby reducing total maintenance costs throughout the equipment lifecycle.
Third, systematic operator and maintenance training can help companies improve equipment utilization and safety. Manufacturers can provide professional training covering equipment operation, safety procedures, routine maintenance, and troubleshooting to standardize operating practices and extend equipment service life.
Fourth, long-term maintenance services should include regular inspections, equipment commissioning, software or firmware updates, and application optimization. Such services enable manufacturers to continue supporting customers as warehouse capacity expands and operational requirements evolve.
5. Industry Experience, Market Reputation, and Proven Application Cases
Experience with narrow aisle reach truck applications cannot be developed overnight. Manufacturers need long-term involvement in industries such as warehousing and logistics, smart manufacturing, cold-chain storage, and automotive parts to accumulate extensive application experience.
Experienced manufacturers can identify potential operating challenges in different environments and address them in advance through product optimization and customized solutions, reducing the risk of equipment being poorly matched to actual working conditions.
A strong market reputation, stable customer repeat-purchase rate, and proven cooperation with industry-leading companies are also valuable indicators of product quality and service capabilities.
Unlike small manufacturers that focus primarily on low-price, high-volume sales, reliable brands tend to place greater emphasis on long-term market reputation. They maintain strict standards for product quality and after-sales service, helping achieve lower equipment failure rates, more manageable maintenance costs, and greater operational stability.
This can help businesses maintain efficient and cost-effective warehouse operations over the long term.
Conclusion
Choosing a reliable narrow aisle reach truck manufacturer is not simply about finding the lowest price. Businesses should evaluate manufacturers across five key dimensions: technical adaptability, manufacturing reliability, customization capabilities, service coverage, and industry expertise.
A manufacturer with independent R&D capabilities, precision manufacturing processes, scenario-based warehouse solutions, and comprehensive full-lifecycle after-sales support is better positioned to provide stable, safe, and efficient equipment for high-density warehousing operations.
The right manufacturing partner can do more than supply a forklift. By matching equipment capabilities with actual warehouse requirements, it can help businesses continuously reduce operating costs and accelerate the transition toward smarter, more space-efficient, and more integrated warehouse operations.